Josch Strahlschweisstechnik GmbH
 Germany, 06193 Götschetal OT Teicha
Overview
About Josch Strahlschweisstechnik GmbH
Who we are
We are your service provider in the following sectors
Electron beam welding
Electron beam hardening
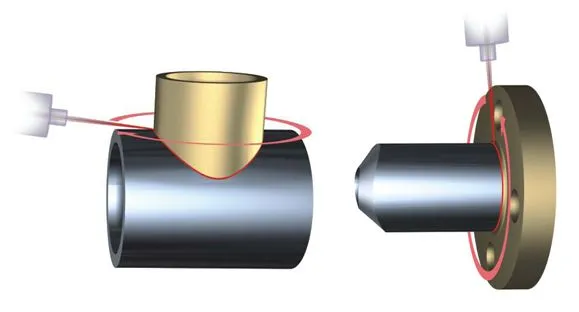
Laser welding
Design meeting the requirements of electron beam welding
Development of electron-beam welding equipment
Electron beam welding totally annuls the classical requirements like:
Same material,
Same material thickness,
Low heat conduction,
Low content of companion elements and
Low carbon content.
The reason for that are the narrow deep seams and the high process speeds. Therefore, this method is not limited to standard materials but may also be successfully applied to special materials, various material combinations, thin-walled and thick-walled structures. Economic solutions are always based on designs meeting the requirements of electron beam technology since the technological advantages of electron beam engineering, weld joint testing and savings in the processing operations are combined.
The clever and extremely cost-saving component design simply uses the specific features inherent to electron beam welding:
Narrow weld seams due to energy input = 1% in comparison with TIG or MAG seams - resulting in minimum shrinkage and minimum distortion
Narrow heat-affected zone - permits relief of welding stresses through equalisation with the elasticity of basic material
1 / 2
2 / 2
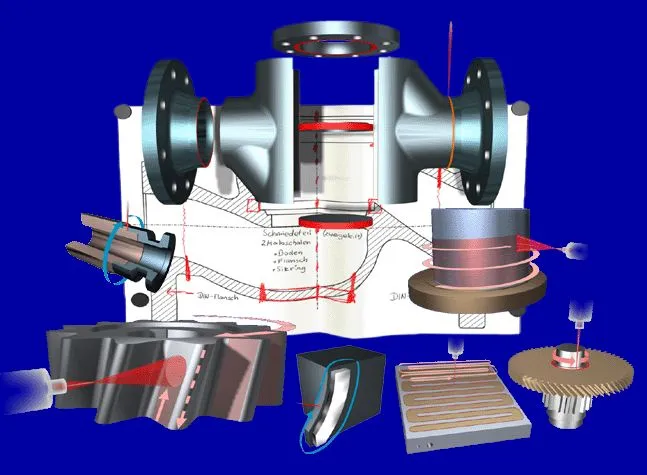
Götschetal OT Teicha, Germany
Member since 2001
Employees20 - 50
Turnover1 - 5 Mil.
Year of foundation1998
Competencies
Technologies
Measuring & Testing
| Technologies | Length | Width | Height | Diameter | Weight |
|---|---|---|---|---|---|
Measuring / testing | 1–1,500 mm | 1–1,500 mm | 1–1,500 mm | 1–500 mm | 0–750 kg |
Welding
| Technologies | Lotsize | Length | Width | Height | Diameter | Weight | Material thickness |
|---|---|---|---|---|---|---|---|
Laser-beam welding | 1–50,000 | 5–1,900 mm | 1–1,300 mm | 5–1,000 mm | 1–500 mm | 0–800 kg | — |
Electron-beam welding | 1–50,000 | 5–1,900 mm | 1–1,300 mm | 5–1,000 mm | from 0 mm | 0.001–800 kg | from 0 mm |
Heat Treatment
| Technologies | Lotsize | Length | Width | Height | Diameter | Weight | Material thickness |
|---|---|---|---|---|---|---|---|
Induction hardening | 10–500 k | 5–400 mm | 3–100 mm | 5–400 mm | 3–100 mm | 0–75 kg | from 0 mm |
Materials
Precious metals
SilverGoldPlatinumOther precious metals
Cast metals
Cast steel
Light metals
Aluminium and aluminium alloysMagnesium and magnesium alloysTitanium and titanium alloys
Heavy metals
Copper-zinc alloys (brass)Copper and copper alloysZinc and zinc alloysSolder
Steel
Structural steelCase hardening/tempering steelStainless steel (rust-proof V2A)Free-cutting/mild steelTool steelCold extruding steel
Advanced Materials
Nickel alloy (Inconel, Monel, Hastelloy)
Industries
Special purpose machinery manufacturingPackaging industryAutomotive and vehicle constructionDrive and gear engineeringApparatus engineeringFittings engineeringBoiler, container and tank construction Shipbuilding industryHydraulic and pneumatic industryMining and tunnel engineeringMachine tool manufacturingChemical industryElectrical industryPower generation and transmission industryMechanical engineeringRailway and rail vehicles industryPaper and printing machinery industryPlant engineering and constructionAerospace and aviation industryAir conditioning, refrigeration and ventilation industryMedical technologyMilitary engineering
Parts & Machines
Parts (12)
1 / 12
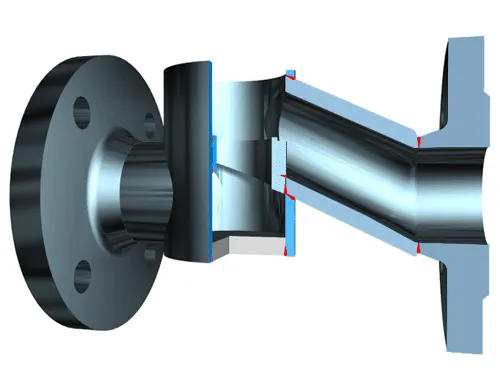
Durchgangsventil
DescriptionMittelteil bestehend aus Rohr-in-Rohr-Schweißung, spaltkorrosionsfrei eingeschweißter Sitz aus Edelstahl
2 / 12
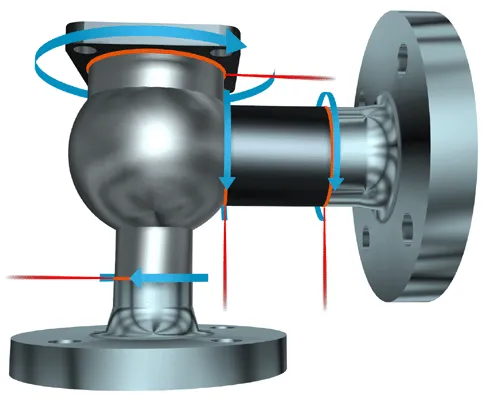
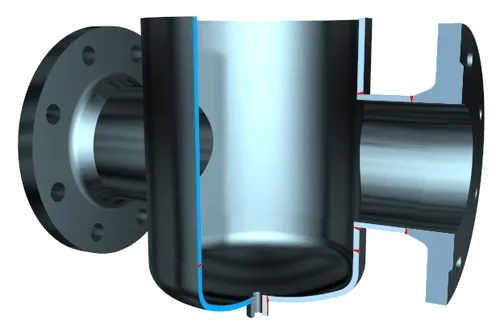
Eckventil
DescriptionElektronenstrahlgeschweißt aus Stabmaterial, Rohr, Flachmaterial und DIN-Flanschen
3 / 12
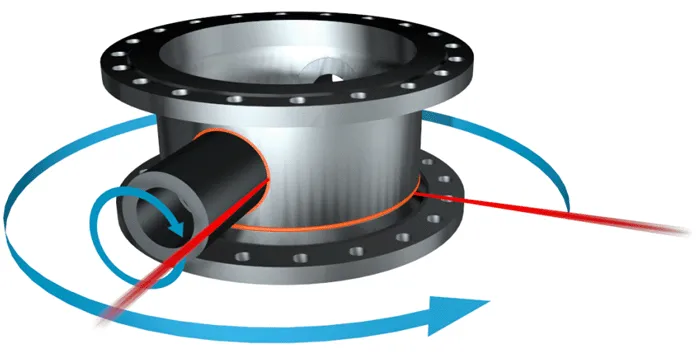
4 / 12
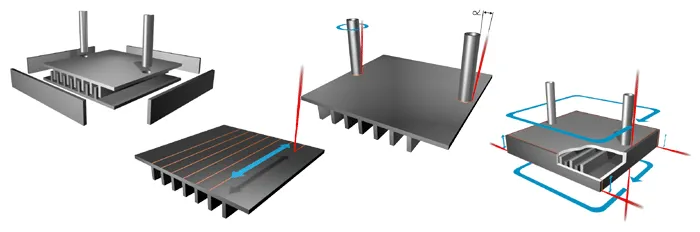
Wärmetauscher aus hochschmelzendem Metall
DescriptionMinimaler Materialeinsatz, minimale Bearbeitungszeiten
5 / 12
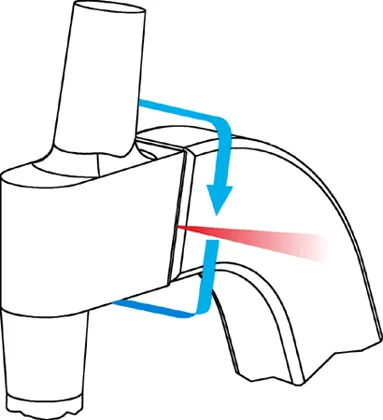
Schweißen von geschmiedeten Titan-Bauteilen
DescriptionZweck: Ablösung kostenintensiver Schmiedung aus einem Stück
6 / 12
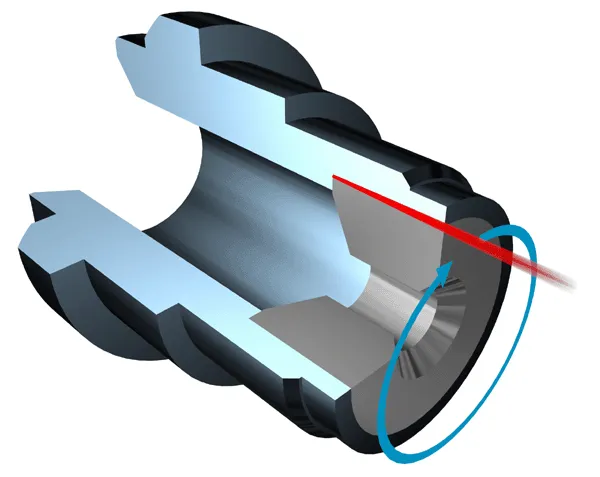
Schweißen von Stellite 6 mit Edelstahl
DescriptionZweck: Ablösung von Stellite-Aufschweißungen
7 / 12
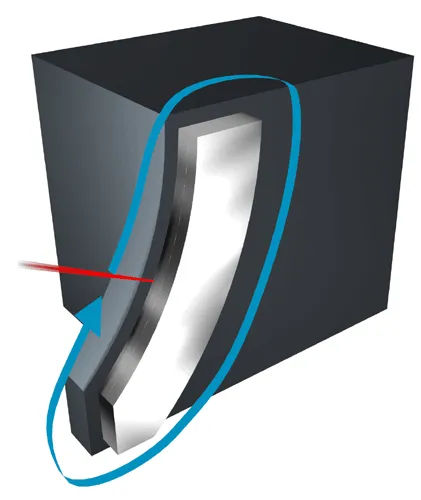
Schweißen von Platin mit Titan
DescriptionZweck: Einsparung von Platin
8 / 12
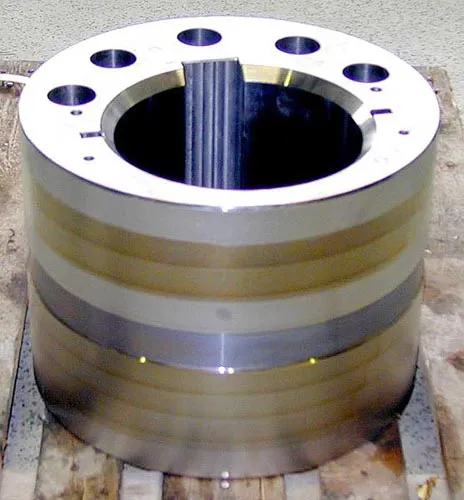
Exzenterbuchse
DescriptionHärten einer Exzenterbuchse 0,8 mm tief, GGG 60
9 / 12
10 / 12
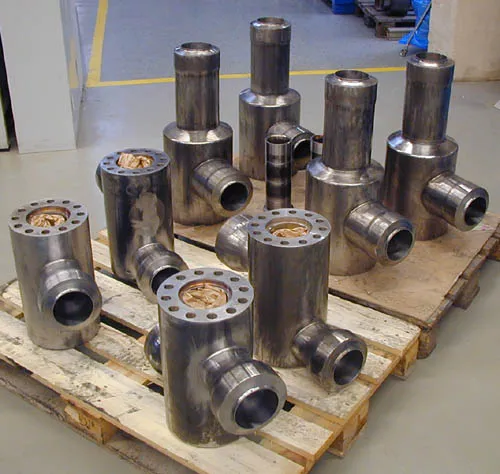
Eckventilgehäuse
DescriptionEckventilgehäuse für Kraftwerke 3D-Stutzenschweißung
11 / 12
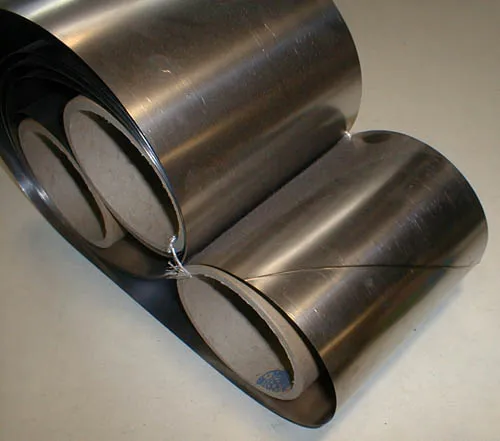
Förderbänder
DescriptionElektronenstrahlschweißung von Förderbändern, 0,2 mm
12 / 12
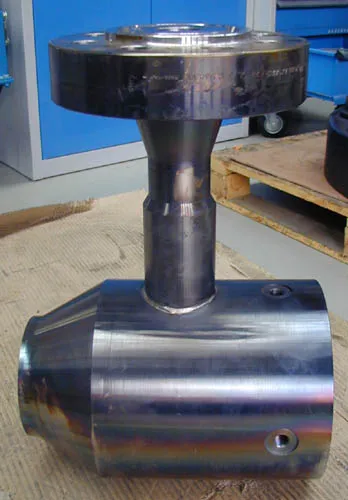
Gehäusebauteil
DescriptionBauteil für ein Stellventilgehäuse
Machinery (2)
1 / 2
xx
ManufacturerPTR
ControlSiemens
Year of Construction2000
Technology
Electron-beam welding
2 / 2
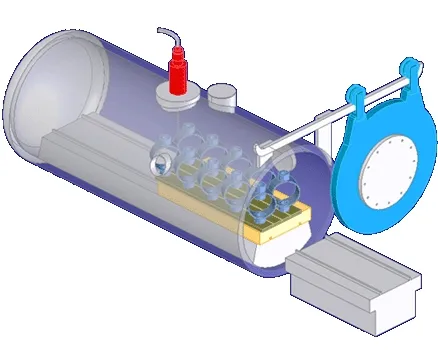
Josch II
ManufacturerPTR
ControlSiemens
Year of Construction2000
Technology
Electron-beam welding
12 Parts
2 Machinery
Electron-beam welding2
Contact
Location
Main locationDorfplatz 9, 06193 Götschetal OT Teicha, Germany
Further locations06193 Teicha, nähe Halle (Saale)
Bundesland: Sachsen-Anhalt
Region: Saalkreis
Verwaltungssitz: Merseburg
Bundesland: Sachsen-Anhalt
Region: Saalkreis
Verwaltungssitz: Merseburg
Company contact
Contact persons
JS
Joachim Schenke
Are you a supplier?
Find perfectly matching requests.
Are you a buyer?
Submit your request.